Production band sawing
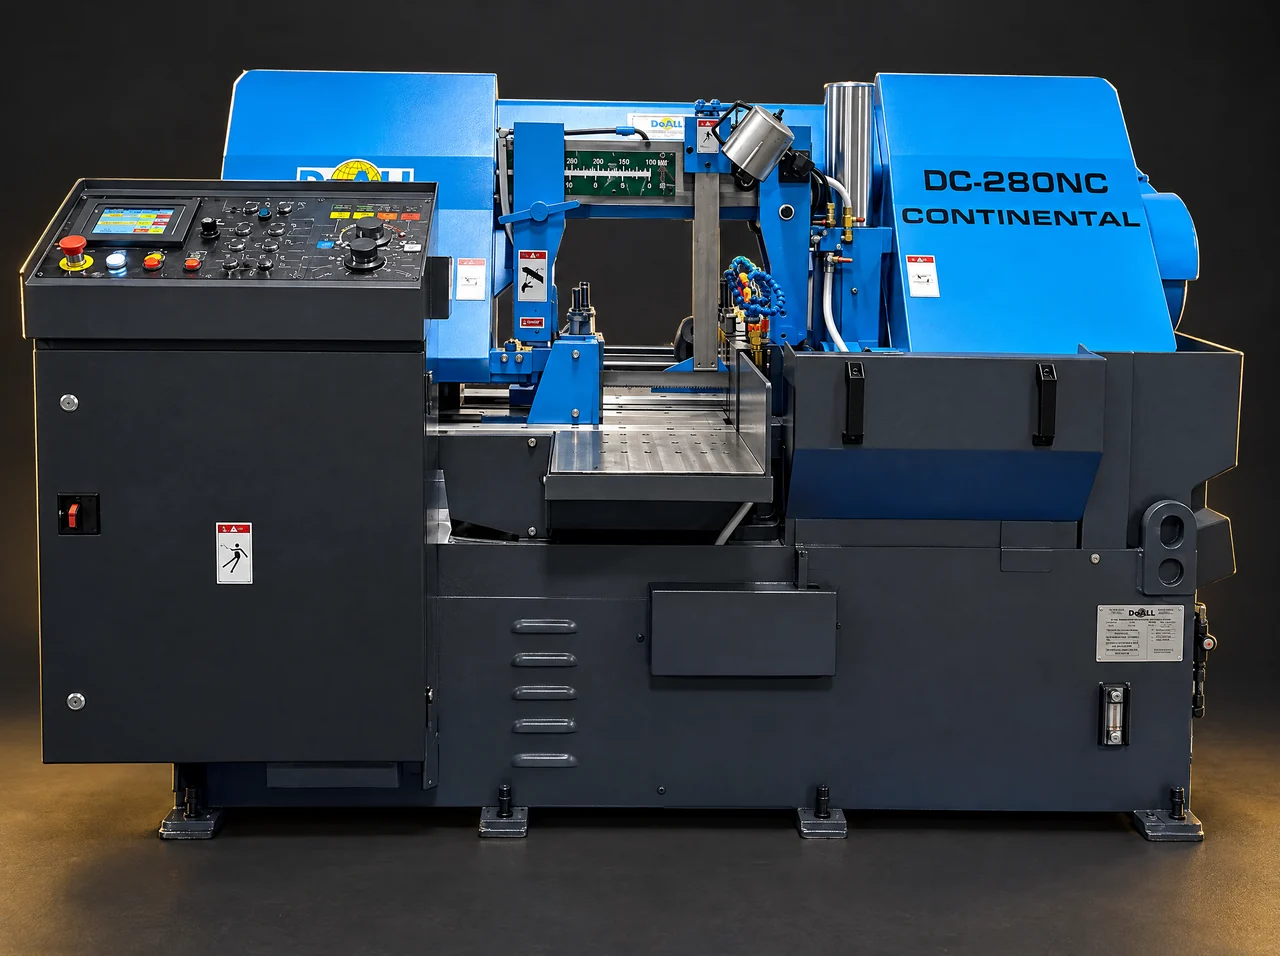
DoALL DC-280NC
Our DC-280NC bandsaws support repeat cutting of metal bar stock into blanks for threaded products and machined components.
DoALL and Behringer sawing. Landis threading. Doosan CNC machining. Dedicated finishing and identification equipment, working together in Houston.
Dedicated band and cold saws prepare bar stock for the threading and machining operations that follow.
Our DC-280NC bandsaws support repeat cutting of metal bar stock into blanks for threaded products and machined components.
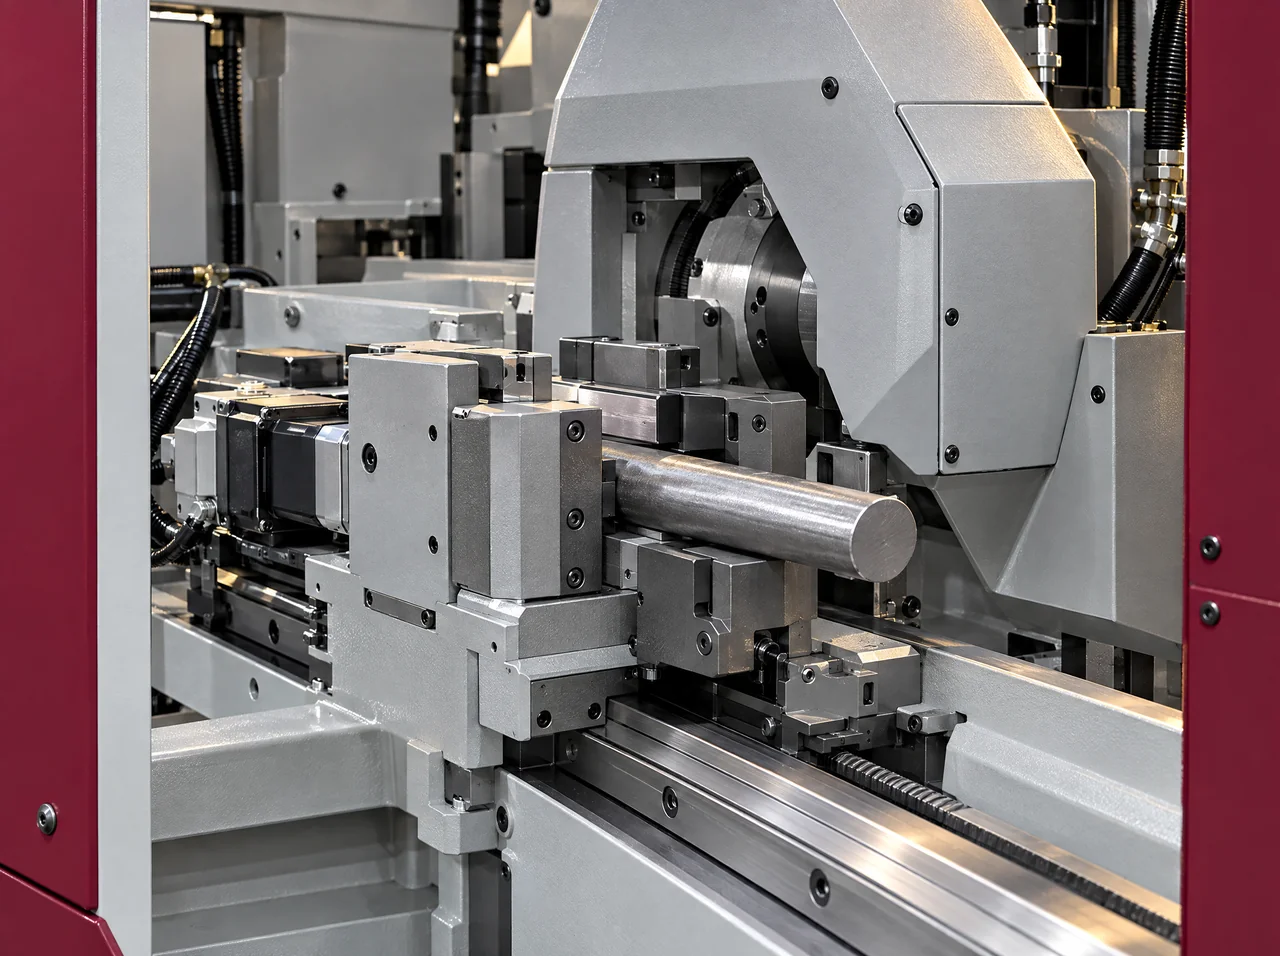
A dedicated circular cold saw supports production cutoff work, preparing consistent blanks for downstream manufacturing.
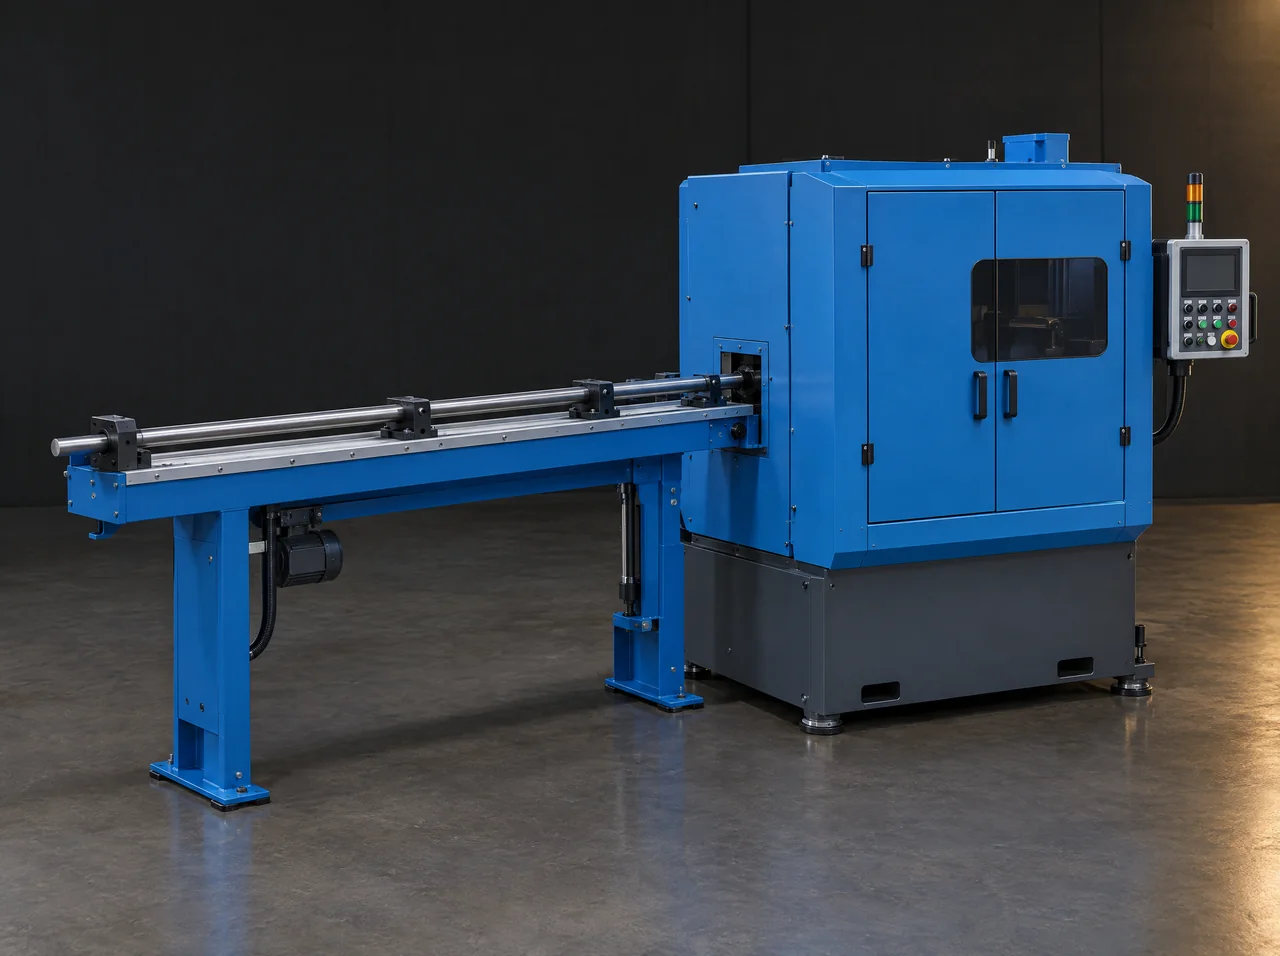
The SC-75A complements our cold-saw capacity for repeat bar-stock cutting and production blank preparation.
A fleet of Landis cut-thread machines, in single-head and double-head configurations, works alongside dedicated Landis roll-threading equipment.
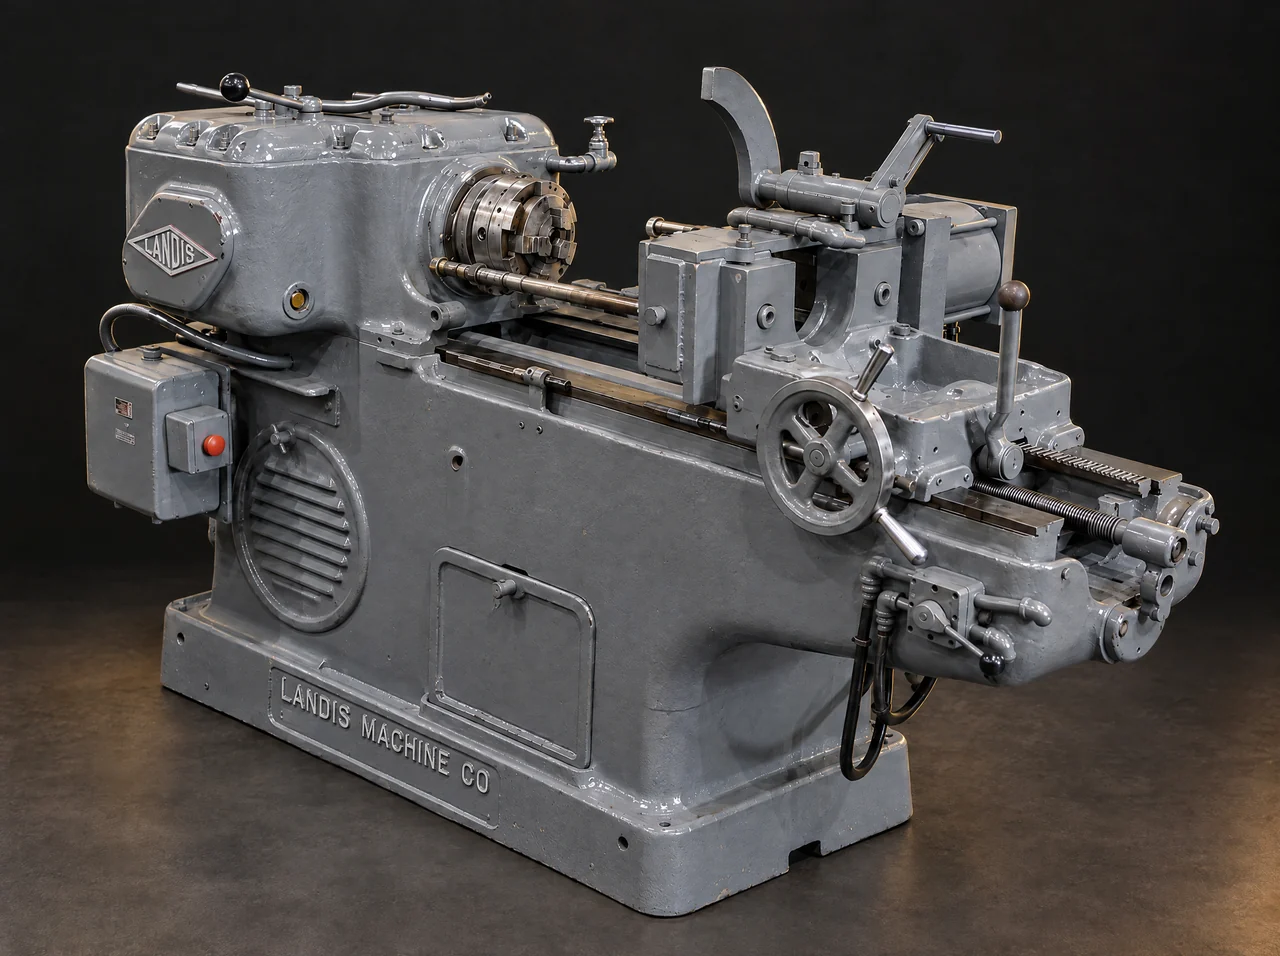
Dedicated cut-thread equipment machines external threads to the form, pitch, class and length specified for the component.
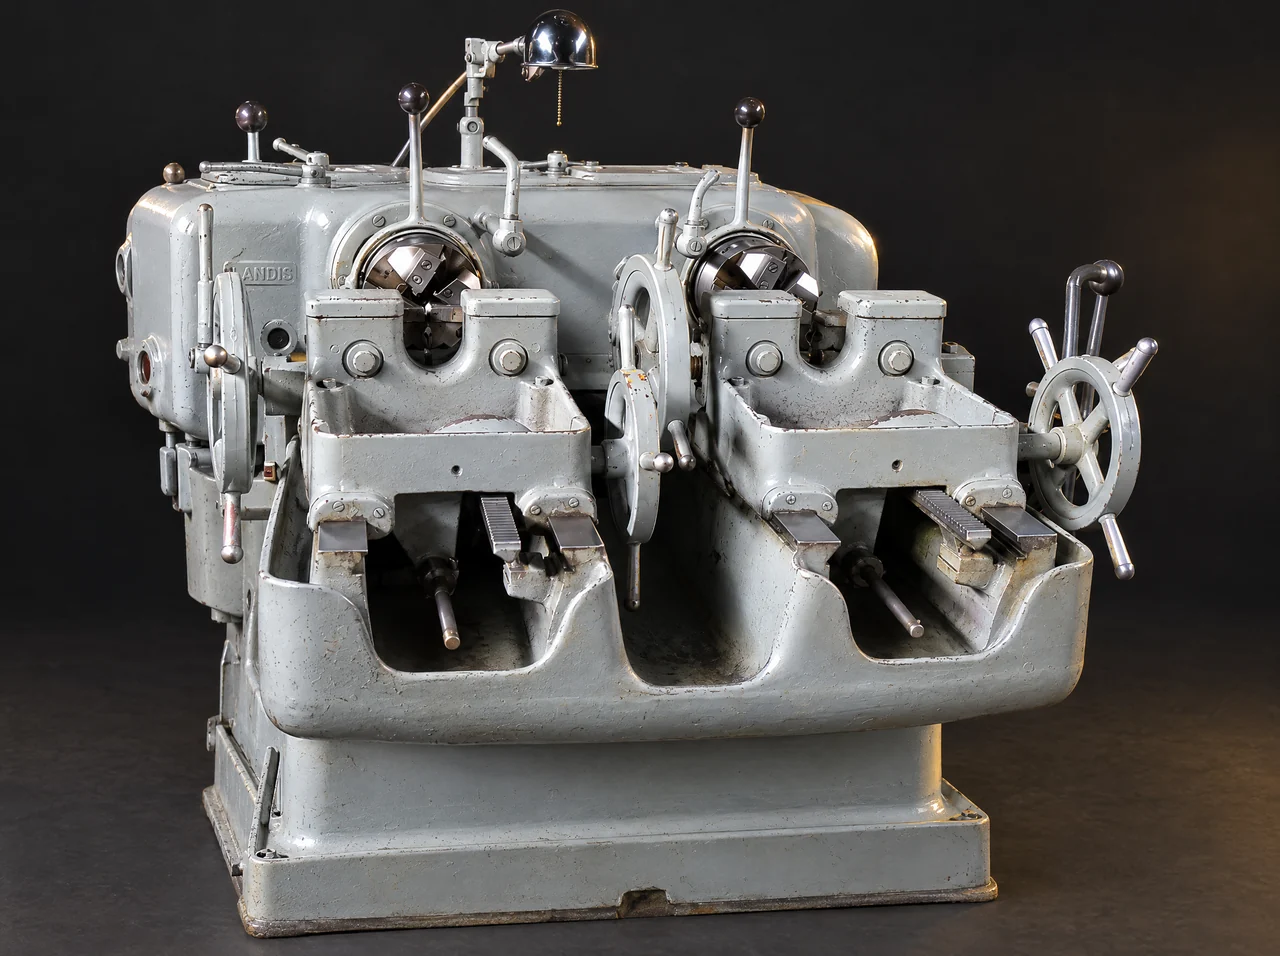
Double-head machines complement our single-head fleet for stud and threaded-product production. The setup follows the end and overall-length requirements of the part.
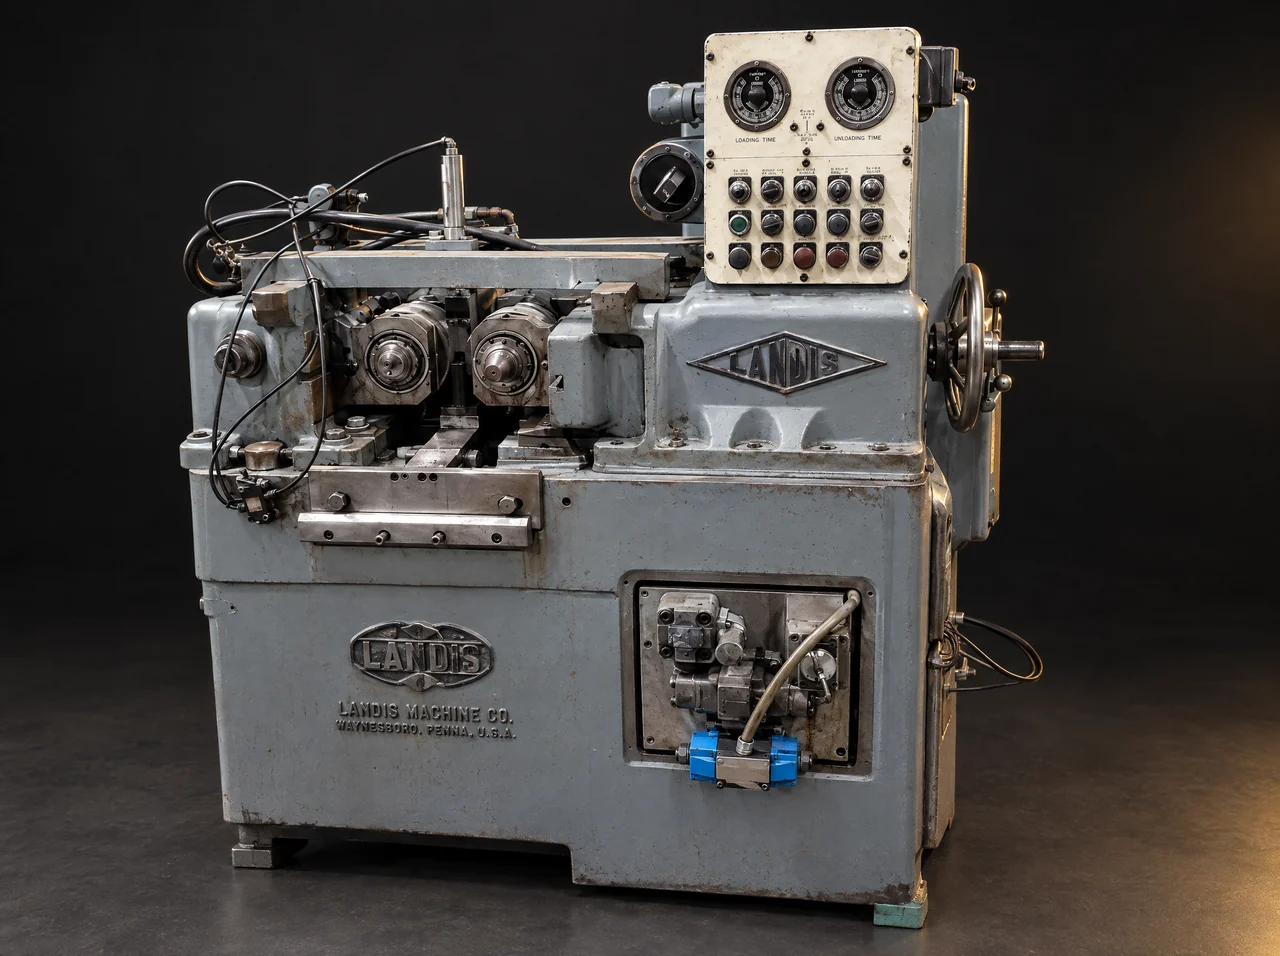
Thread rolling forms the external thread with rolling dies. Material condition, blank diameter and thread requirements determine the manufacturing route.
Our CNC fleet is all Doosan: multiple PUMA and Lynx turning centers, supported by a vertical mill for drawing-controlled components.
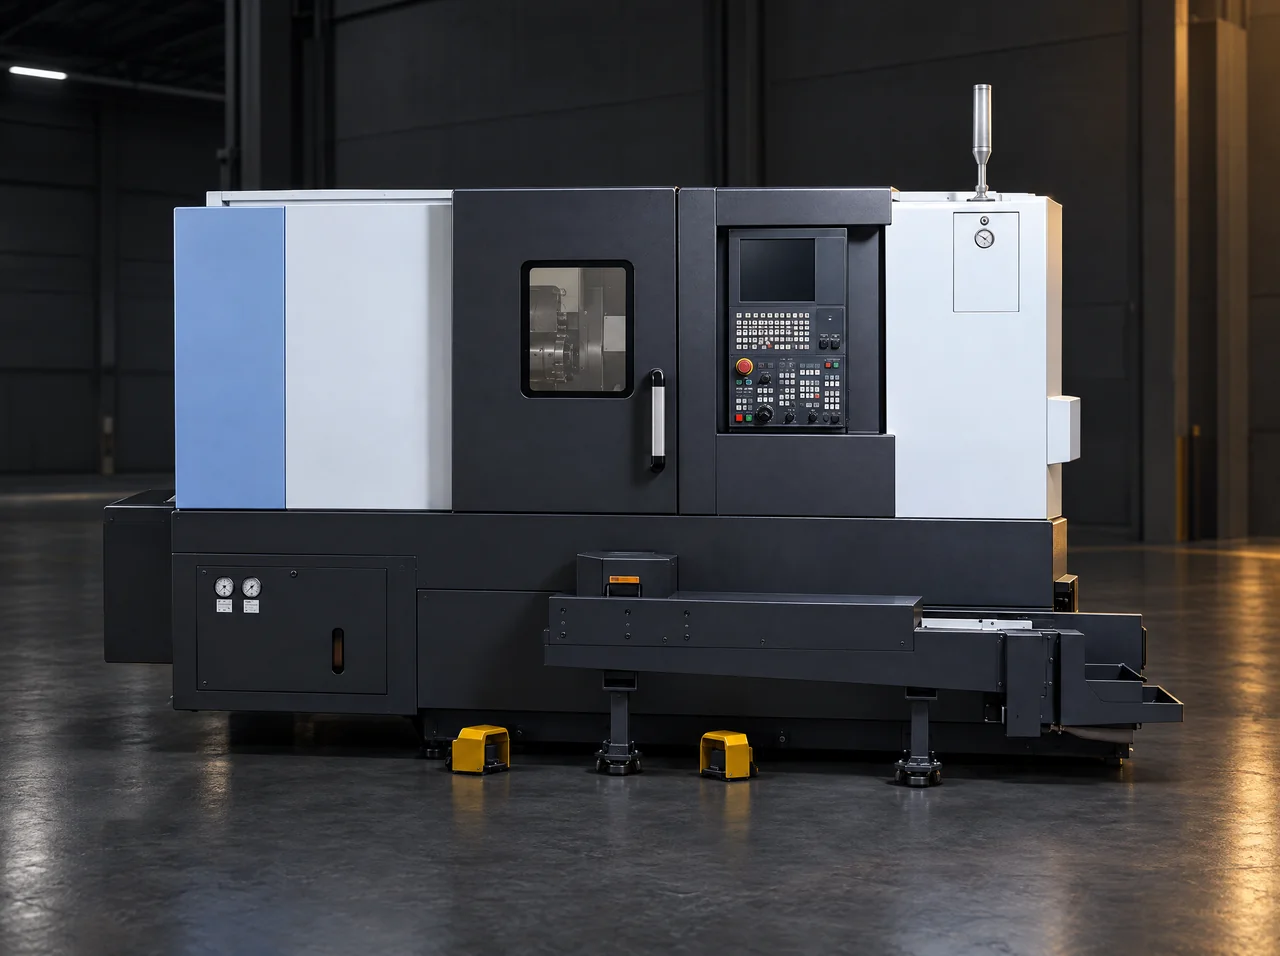
PUMA equipment supports turned diameters, shoulders, grooves and threaded features, with live-tool operations reviewed against the drawing.
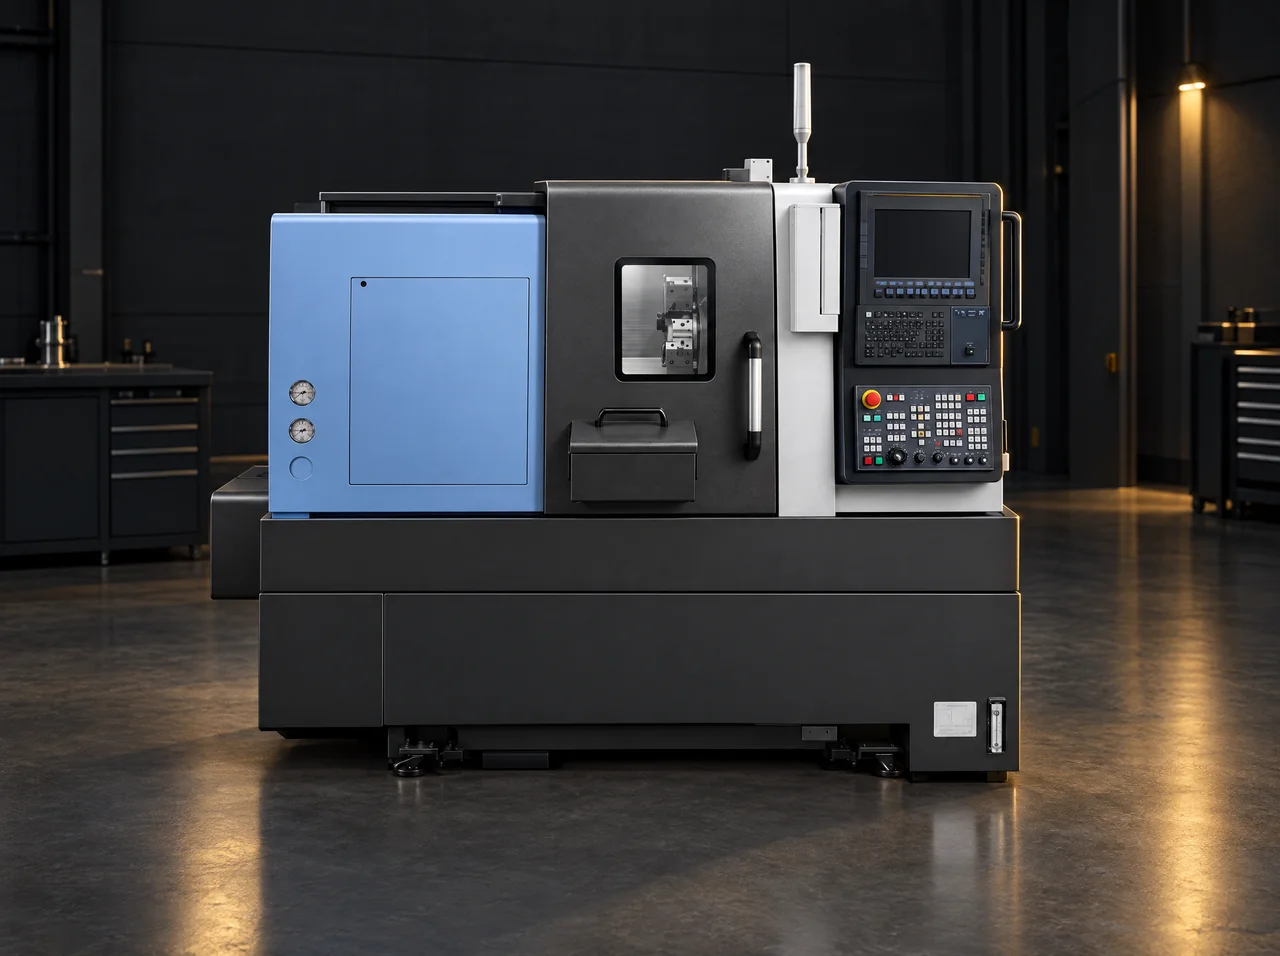
Our Lynx machines add flexible turning capacity for fasteners and custom components, from part setup through repeat production.
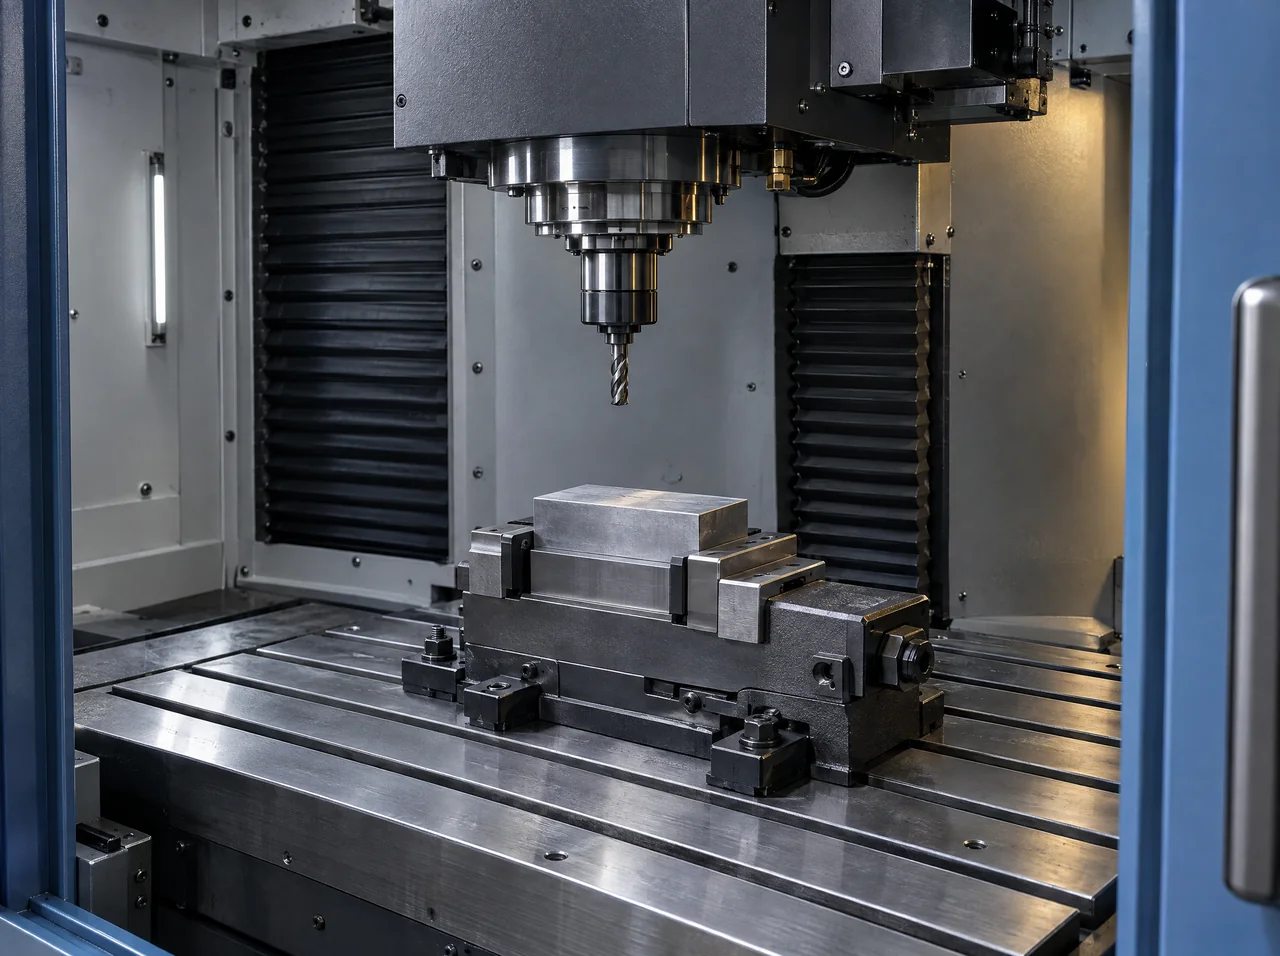
Vertical milling complements our turning operations for flats, holes and other drawing-defined features on custom manufactured parts.
Dedicated finishing and marking equipment carries the component through end preparation, internal threading and permanent identification.
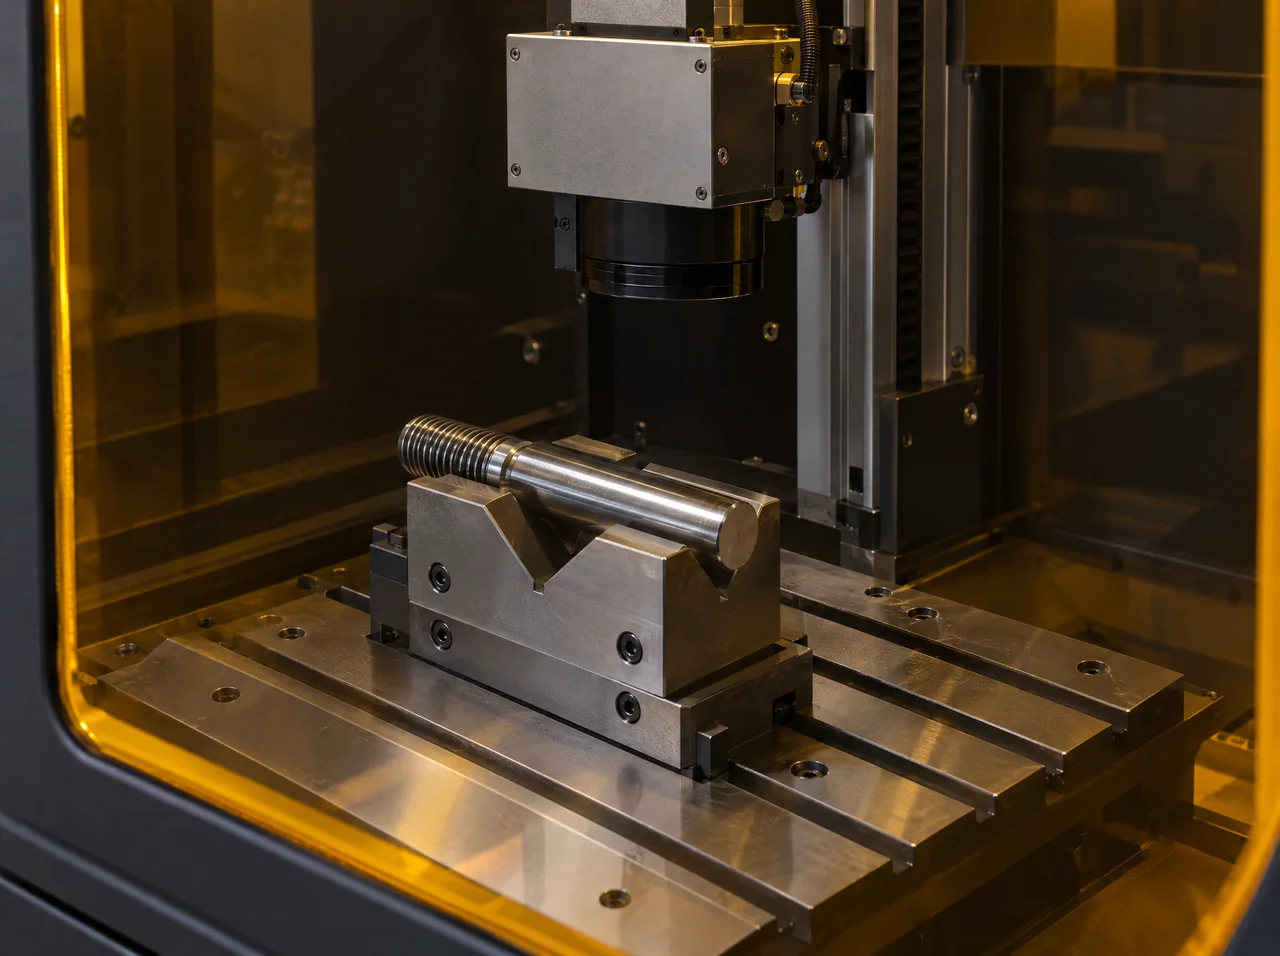
Laser marking applies the identification specified for the order. Mark content, position and legibility are defined with the part requirements.
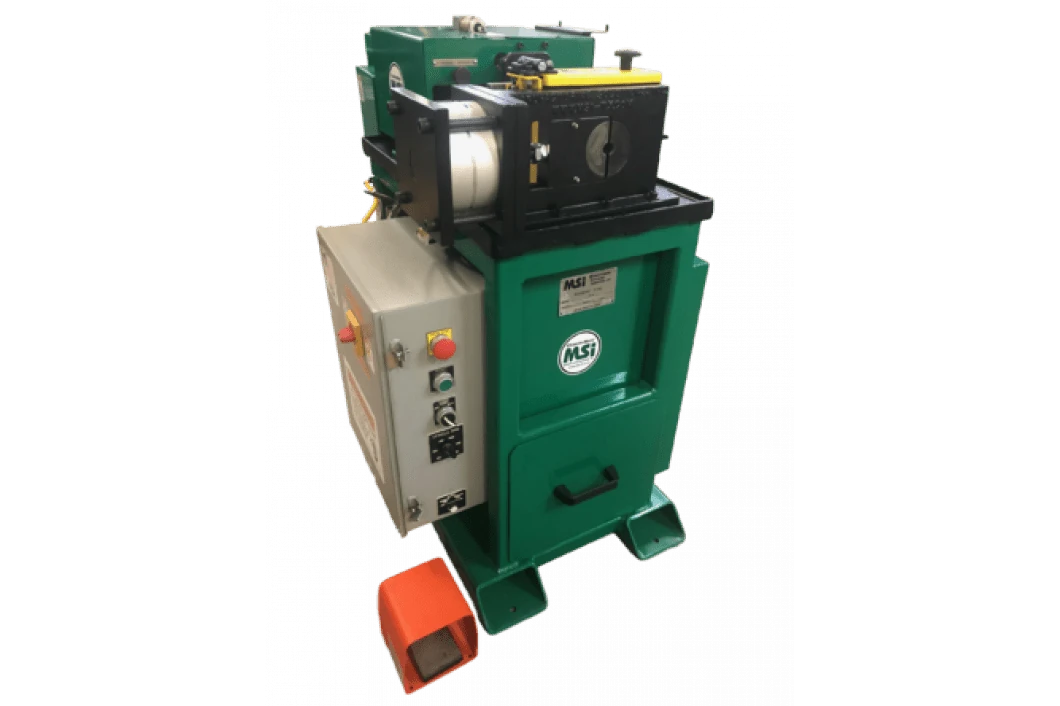
Our MSI ChamferMate machines prepare stud and bolt ends to the required edge geometry. The C3A-M combines chamfering and end marking in a compact machine, with operations selected for the part.
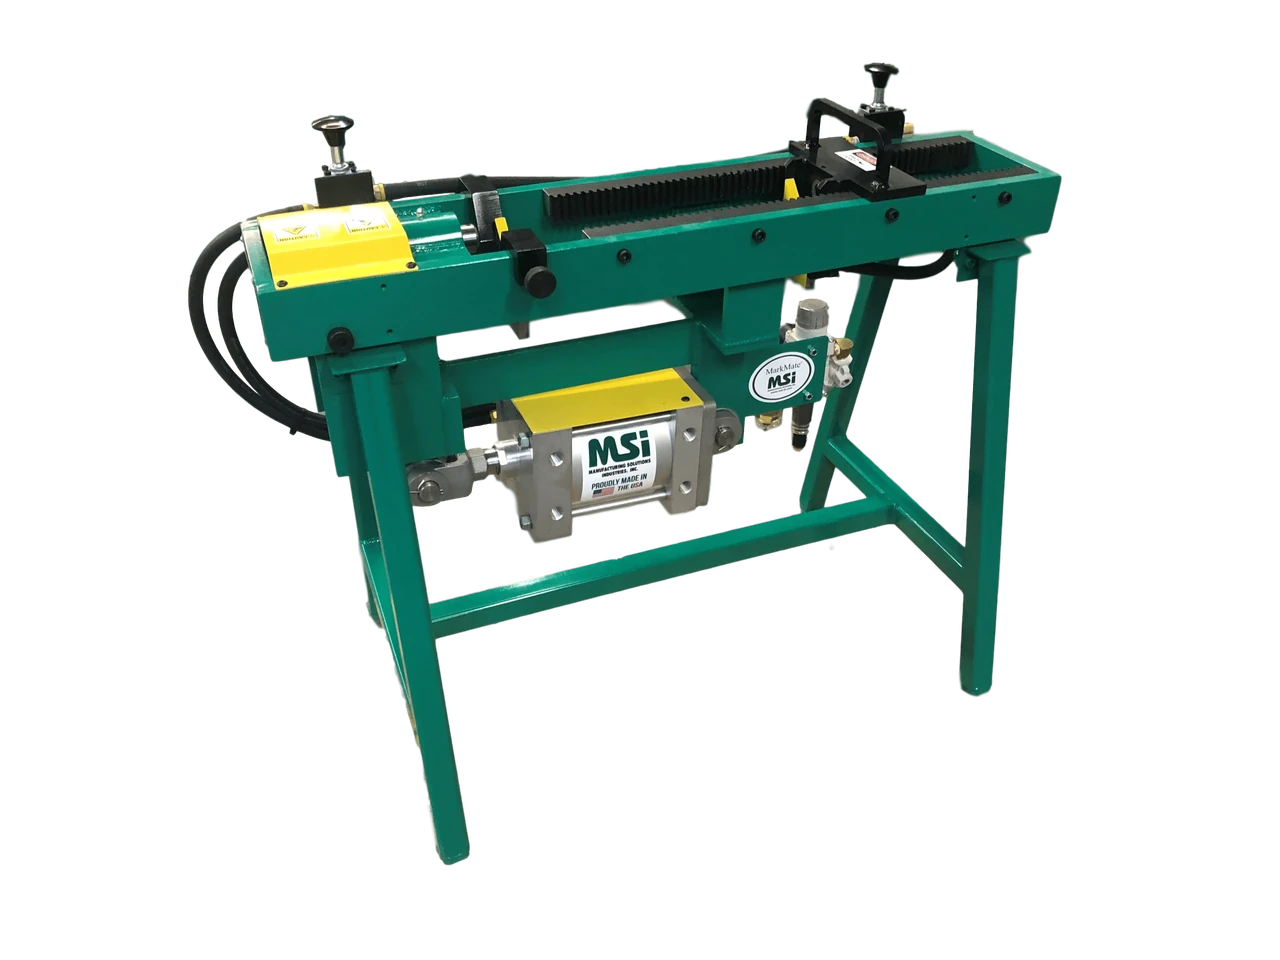
The MSI MarkMate applies impressed identification to the ends of studs, bolts and shafts. Adjustable part supports accommodate the required setup, with mark content and location defined by the order.
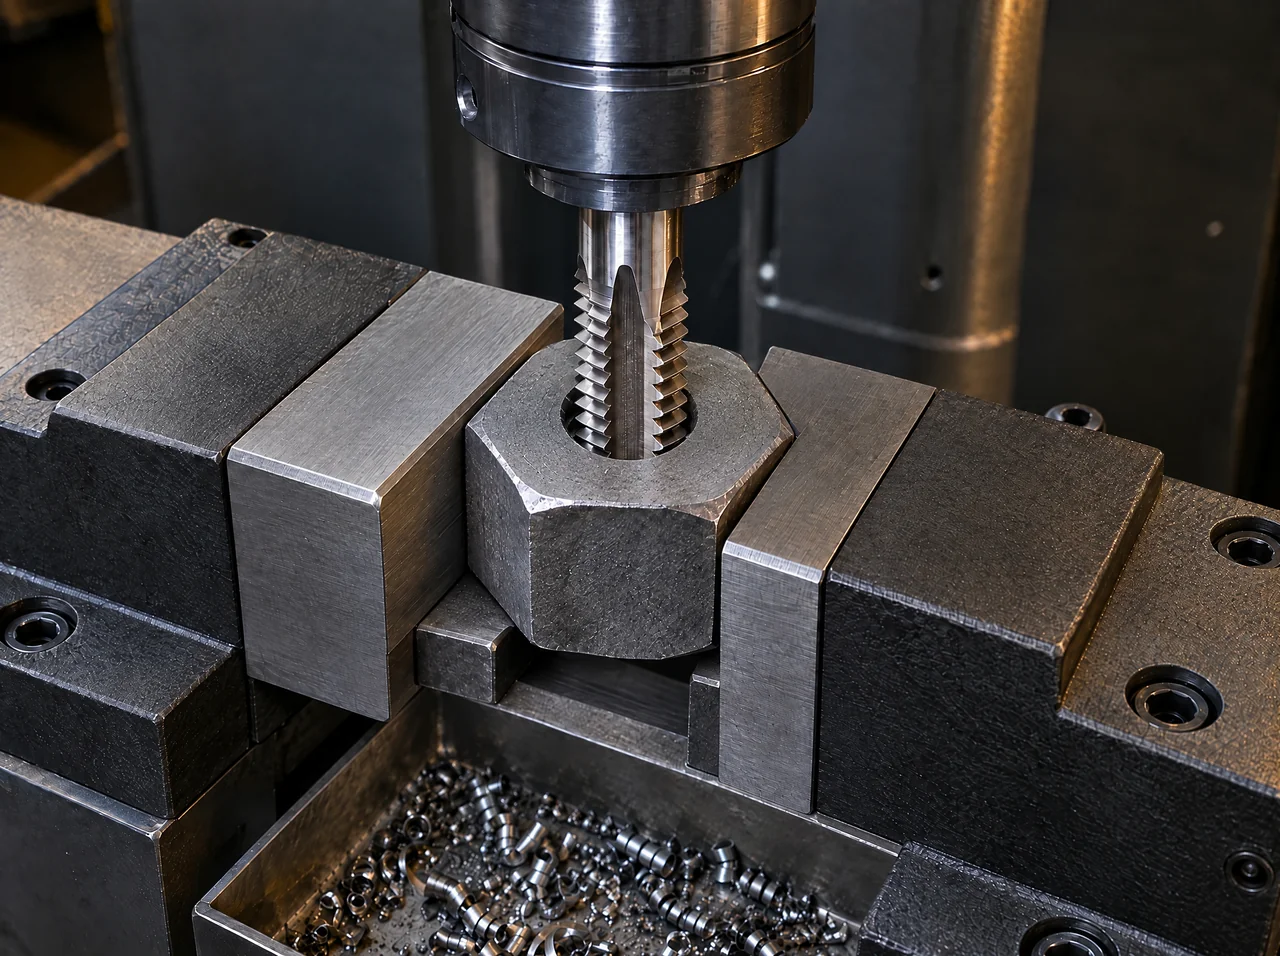
Dedicated drill-press tapping setups produce internal threads in nuts, complementing our external-thread manufacturing capabilities.
Supporting systems are part of the manufacturing operation, too.
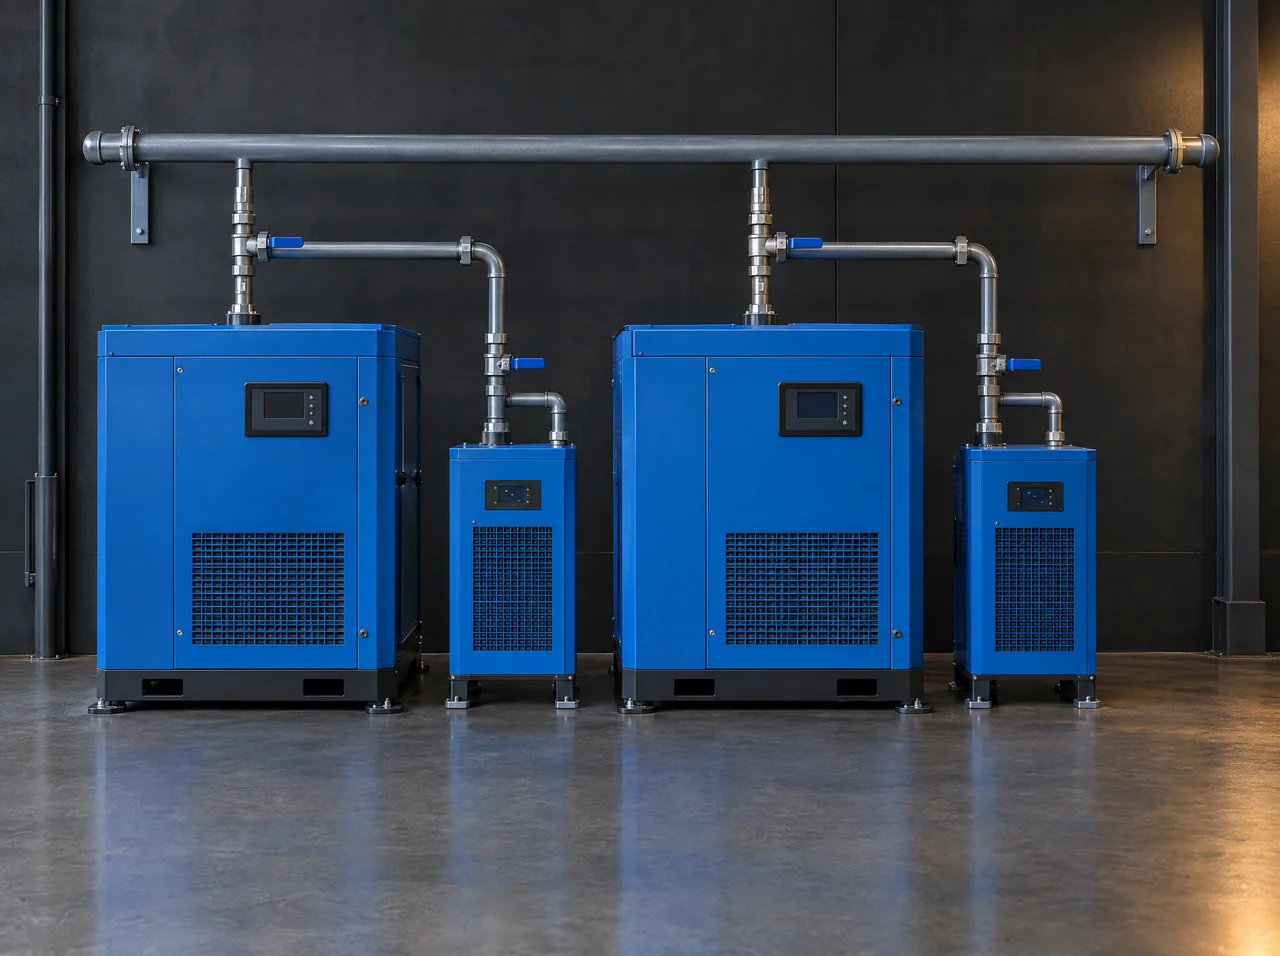
Two Quincy air compressors with dryers support the shop’s pneumatic equipment and manufacturing operations.
Send the part geometry, material condition, thread specification, quantity and acceptance criteria together.
Our team reviews the manufacturing route, workholding, inspection and documentation requirements for your component. Machine envelopes and achievable tolerances are confirmed during that review.
General machining reference values. Material, geometry, setup and inspection requirements determine the tolerances quoted for a specific order.
| Operation | Standard Tolerance | Precision Tolerance | Measurement Method |
|---|---|---|---|
| CNC Turning (Diameter) | ±0.005" | ±0.001" | Micrometer |
| CNC Turning (Length) | ±0.010" | ±0.002" | Caliper, Height Gauge |
| Threading (Pitch Diameter) | ±0.003" | ±0.0005" | Thread Gauge, Optical |
| Surface Finish (Ra) | 63 μin | 16 μin | Profilometer |
| Concentricity/Runout | ±0.005" TIR | ±0.001" TIR | Dial Indicator |
| Perpendicularity/Squareness | ±0.003" | ±0.0005" | Square |
Reference topics from our published machining information. Confirm the thread form, material, features and documentation required for your specific component with the Cyclone team.
Tell us what you need to manufacture. We’ll review the requirements, documentation, and delivery together.